MESSAGE
If you have any questions, please contact us and we will contact you as soon as possible.
‹
›
‹
›
◉ PRODUCT SPECIFICATION
Product Description
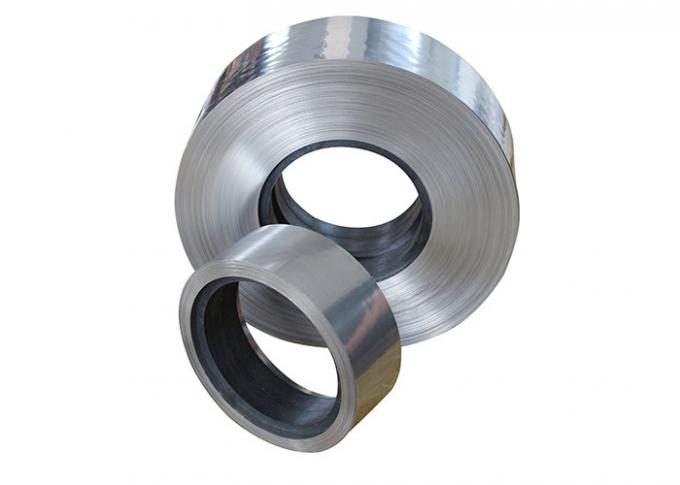
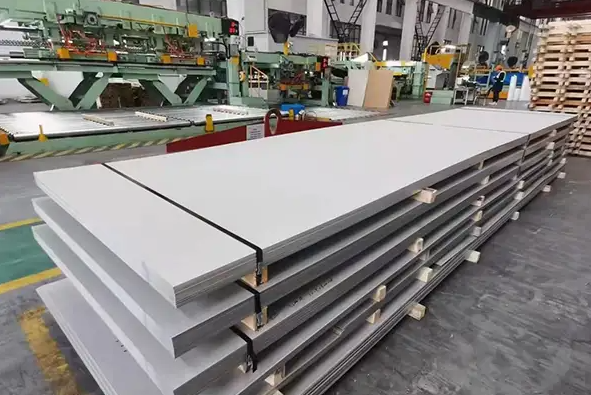
Nitronic 60 is a high Silicon, high Manganese, Nitrogen strengthened austenitic stainless alloy. Nitronic 60 is an all purpose metal that was originally designed as a temperature alloy and therefore performs well at high temperature around 1800ºF. The additions of silicon and manganese assist to inhibit wear, galling and fretting even in the annealed condition. Through cold working Nitronic 60, it is possible to attain higher strengths, however it does not enhance the anti-galling properties. The oxidation resistance of Nitronic 60 is similar to Alloy 309 and far superior to Alloy 304.
Nitronic 60 is used in the Aerospace , Food and Drug, Oil Field, Petrochemical, Surgical and Chemical Processing Industries.
Common Trade Names:
Nitronic 60 / UNS-S21800 / Alloy 218 stainless steel
Specifications:
ASTM A193 / A194 / A240 / A276 / A314 / A479 /A351 / A7430
Nitronic 60 Chemical Composition
Nitronic 60 Physical Properties (Annealed )
Nitronic 60 Typical Mechanical Properties
Corrosion Resistance
The uniform corrosion resistance of Nitronic 60 falls between grades 304 and 316. However, in a wear system, galling or seizure occurs first, then dimensional loss by wear, and finally corrosion. Galling and wear are the first concerns in design. Although the uniform corrosion resistance of Nitronic 60 is not quite as good as 316, it offers better pitting resistance to chlorides, stress corrosion cracking resistance and crevice corrosion resistance than grade 316.
Fabrication and Heat Treatment
Fabrication
Nitronic 60 can be hot forged. After forging the workpiece must be solution annealed.
Machinability
The alloy is difficult to machine, rated at 50% of 304 and 23% of the free cutting carbon steel AISI B1112. Sharp, rigid, carbide tipped tools and well powered machines are recommended, with the use of heavy cuts and slow speeds.
Heat Treatment
Nitronic 60 is fully austenitic and can not be strengthened by heat treatment. Solution annealing is carried out at 1060°C, followed by water quenching
Weldability
Nitronic 60 is readily welded by all conventional processes. Autogenous GTAW welds are sound, with wear characteristics approximating to the base metal. GTAW welds in heavy sections are also sound and weld tensile strength is slightly higher than base metal. Wear properties are near but below base metal. Pure argon is used as shielding gas and AWS A5.9 ER 218 filler metal is used. Pre-heating and post heating are not needed.
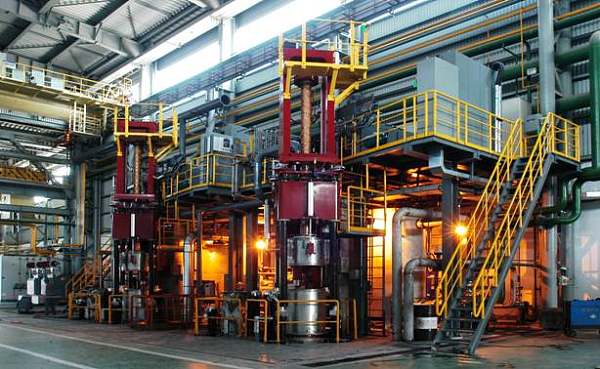
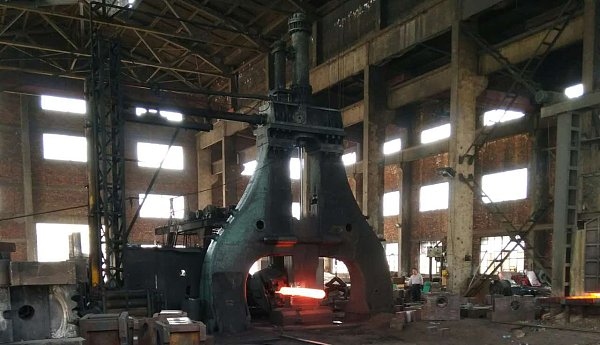
◉ Factory Show
◉ MESSAGE
◉ SIMILAR RECOMMENDED
 ERNiCrMo-3/UNS N06625/W. Nr. 2.4806 AWS A5.14 Wire
 Super Invar 32-5 Sheet Plate 4J32/K93500/Super Invar Sheet Plate
 NILO 4J36 Tube Pipe UNS K93600 & K93601/W. Nr.1.3912 Ultra-low expansion iron-nickel alloy Tube Pipe
 Hastelloy Alloy B-3/UNS N10675/W. Nr. 2.4600
 Monel Alloy 400/UNS N04400/W.Nr. 2.4360
 Incoloy 800/Alloy 800/UNS N08800/W.Nr. 1.4876
 Inconel 625 Alloy | Nickel Alloy 625 Supplier and Manufacturer
 Inconel 718 Alloy | UNS N07718 Nickel Superalloy Supplier
 17-4PH UNS Strip Ring S17400/W.Nr:1.4542 stainless steel Strip Ring
 AL-6XN Stainless Steel / N08367 /
 PH13-8 / S13800 / W.Nr 1.4534 /Alloy 13-8 stainless / PH13-8 Mo
 F55 Duplex Stainless Steel
") F44 (254 SMO )
 17-7PH / 1.4568 Stainless Steel /631 Precipitation Hardening Stainless Steel
 Nitronic 60 / UNS S21800 / Alloy 218 stainless steel
 Nitronic 50
 904L Stainless Steel
 CuNi1 Wire 210 MPA 0.03mm Soft Copper Aluminium Nickel Alloy
 Bright 420 MPA 50mm Soft CuNi44 Heating Nickel Copper Rod
 0.5mmx180mm Soft MPA CuNi34 Nickel Copper Alloy 400
 CuNi10/CuNi30 Copper Nickel Alloy Strip High Conductivity Corrosion Resistant for Marine & Industrial Use
Thank you very much for writing to us. Please leave your message and contact information, we will reply to you within 24 hours.